How to Choose the Right Welding Electrode for Construction in Pakistan
A step-by-step engineering and practical guide for contractors, site engineers, and fabricators on selecting welding electrodes for Pakistani construction projects.
Direct Answer for Site Engineers & Contractors
Step 1: Identify Your Base Metal Composition
The primary rule in welding metallurgy is to match the mechanical strength and chemical composition of the filler metal to the base metal:
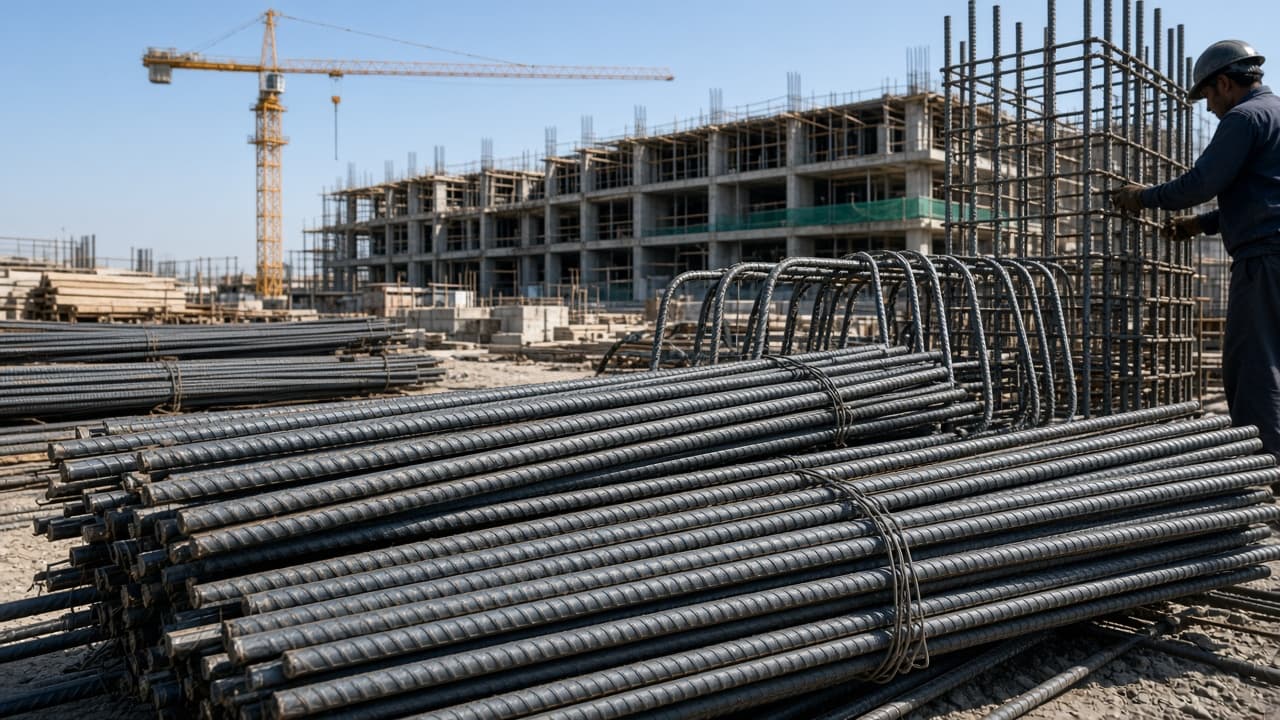
- Mild Carbon Steel (Grade 40/60 rebar, hollow sections, angles, channels, plates):
- High-Yield Deformed Rebar & Thick Structural Flanges (> 25 mm):
- Sheet Metal & Light Gauge Tubes:
Step 2: Match Electrode Diameter to Material Thickness
Selecting an oversized electrode on thin metal causes burn-through and excessive heat-affected zone (HAZ) warping. Selecting an undersized electrode on thick plate results in lack of penetration, slag inclusions, and excessive labour costs:
| Base Steel Thickness | Recommended Electrode Diameter | Operating Amperage Range | Typical Construction Application |
|---|---|---|---|
| Up to 2.5 mm (Thin sheet, light tubing) | 2.5 mm (3/32") | 60 – 85 A | Window grills, door frames, HVAC duct supports, sheet metal flashing |
| 3.0 mm – 6.0 mm (Standard structural steel) | 3.2 mm (1/8") | 90 – 125 A | Roof trusses, purlins, column base plates, bracing members, stairs |
| 6.0 mm – 12.0 mm (Heavy structural steel) | 4.0 mm (5/32") | 130 – 175 A | Crane runway girders, portal frames, heavy warehouse columns, bridge beams |
| 12.0 mm and thicker (Massive plate assemblies) | 5.0 mm (3/16") | 180 – 240 A | Thick splice plates, heavy equipment foundations, multi-pass fillet welds |
Pro Tip: The 3.2 mm electrode is the single most versatile and widely stocked electrode diameter on construction sites across Pakistan.
Step 3: Determine Required Welding Positions
Construction joints frequently require out-of-position welding because structural members are already erected:
- Flat & Horizontal: Easiest positions; allows maximum deposition rate and higher amperage.
- Vertical-Up: Necessary for column splices and wall brackets; requires an electrode that produces a fast-freezing slag shelf to hold the molten weld pool against gravity.
- Overhead: Required for ceiling beams, soffits, and bottom girder flanges.
AWS E6013 electrodes are designated as "all-position" (the "1" in E6013), allowing skilled welders to manipulate the puddle vertically and overhead with a short arc length.
Step 4: Account for On-Site Power Quality & Machine Types
Job sites in Pakistan frequently operate on portable diesel generators or rural grid connections prone to voltage fluctuations:
- Single-Phase Portable Inverters (220V): Need electrodes with low open-circuit voltage (OCV) arc strike capability. E6013 runs exceptionally well on DC inverter machines.
- Traditional Oil-Cooled Transformers (AC): Require electrodes with potassium flux stabilizers. E6013 strikes and restrikes effortlessly on AC without arc outage.
- Engine-Driven Mobile Welder Generators: Benefit from E6013's forgiving voltage tolerance during load shifts.
Step 5: Verify Quality Management & Technical Documentation
Do not purchase welding consumables on price alone. Substandard unbranded electrodes cause weld porosity, cold cracking, and catastrophic structural failures. Always verify:
- ISO 9001:2015 Certification: Assures that raw material sourcing, extrusion concentricity, and quality testing are systematically audited.
- Current Technical Data Sheet (TDS): Shows verified chemical composition, tensile strength, yield strength, and impact values.
- Manufacturer Reputation: Choose established Pakistani manufacturers like Perfect Craft (Pvt.) Ltd. who maintain consistent quality control rather than traders importing spot lots.
Step 6: Enforce Strict Job-Site Storage & Handling Protocols
Even the finest welding electrode will produce porous, brittle welds if allowed to absorb ambient moisture on humid construction sites:
- Keep Original Packaging Sealed: Open boxes only when welders are ready to consume them within the shift.
- Store Off Ground in a Dry Area: Elevate cartons on wooden pallets away from damp concrete floors and external walls.
- Avoid Heavy Rainfall Exposure: Protect electrode storage areas during monsoon seasons in Karachi, Lahore, and Punjab.
- Re-Drying: If E6013 electrodes become mildly damp from high humidity, warm them gently in an electrode drying oven at 100°C–120°C for 30–60 minutes. (Never bake E6013 at high heat).
Summary Checklist for Construction Site Supervisors
| Checkpoint | Recommended Action |
|---|---|
| Base Metal | Mild steel -> AWS E6013 (Perfect Bridge or Perfect King) |
| Common Size | Stock 3.2 mm for 70% of structural work; 2.5 mm for light fabrication; 4.0 mm for heavy plates |
| Brand Selection | Perfect Bridge for general structural; Perfect King for heavy industrial |
| Site Compliance | Request and archive current manufacturer Technical Data Sheet (TDS) |
| Consumable Care | Keep dry, store elevated on pallets, seal unused packets |
Technical Resources & Inquiries
Share this technical resource
Published by Perfect Craft (Pvt.) Ltd., Karachi, Pakistan. For questions or technical verification, reach our engineering desk at [email protected].
Next step
Request current technical documents, check dealer availability, or ask about bulk supply. Every form submission returns a reference ID for follow-up.